Engineered Warehouse Rack Manufacturing Excellence
As global supply chains pivot toward ultra-dense storage, cold-chain resilience, and automated logistics integration, selecting the ideal China industrial rack storage manufacturer requires rigorous evaluation of structural steel integrity, FEA simulation capabilities, surface finishing longevity, and international compliance standards (ANSI MH16.1, EN 15512, FEM 10.2.02). This whitepaper offers procurement managers, structural engineers, and logistics directors actionable guidance for evaluating high-capacity industrial rack systems direct from China.
Featured Industrial Rack Systems & Heavy-Duty Storage Products
Explore our precision-manufactured industrial rack lineup engineered for high-load factory warehousing, cold storage, automated logistics, and heavy material distribution.
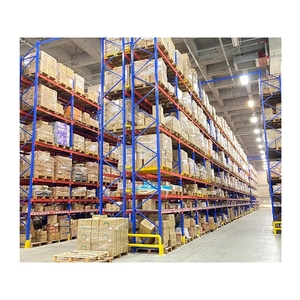
Warehouse Racking System Heavy Duty Industrial Steel Shelving Warehouse Pallet Racks for Sale
Engineered with high-tensile Q235B steel profiles, offering 100% SKU selectivity for dynamic logistics centers.
Get Catalog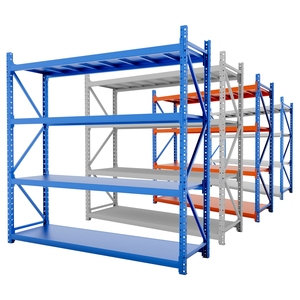
Factory Direct Steel 4Layer/500kg Load Heavy Duty Pallet Rack Bolt Metal Long Span Shelving Industrial Warehouse Storage Racking
Versatile boltless multi-tier longspan arrangement ideal for manual order picking and light industrial parts storage.
Get Catalog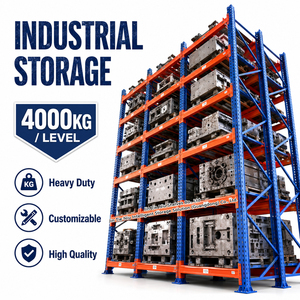
4000KG Heavy Duty Warehouse Rack Pallet Storage System Adjustable Beam Racking
Ultra-heavy beam profiles designed to sustain high static pallet loads up to 4 metric tons per beam level.
Get Catalog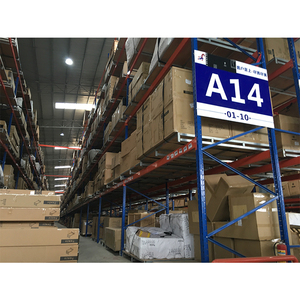
Industrial Storage Rack Heavy Duty Steel Pallet Rack System for Warehouse Organization
Standardized pallet frame geometry compatible with VNA turret trucks and reach forklifts for maximum vertical density.
Get Catalog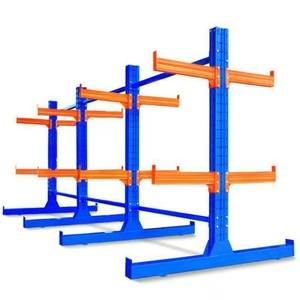
Steel Cantilever Pallet Racking Single Side Heavy Duty Multi-Level Corrosion Protection Garage Use CE Certified 500-3000kg Racks
Unobstructed front arm structure tailored for storing steel pipes, timber bundles, plastic extrusions, and long goods.
Get Catalog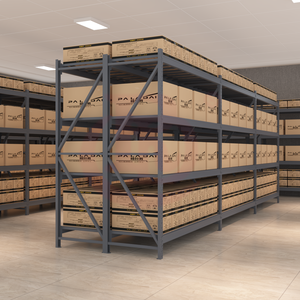
Heavy Duty Mobile Thickened 5 Layer Adjustable Cold-Rolled Steel Pallet Rack with 15m Depth 300kg Load for Factory Materials
Guided track mobile base racking system designed to eliminate fixed aisles and double floor space footprint utilization.
Get Catalog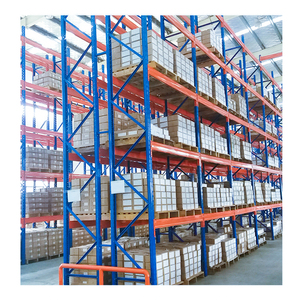
Heavy Duty Industrial Storage Rack Steel Warehouse Pallet Shelving System Supplier
Heavy-gauge industrial frame assemblies engineered for harsh factory operations and high-cycle material handling.
Get Catalog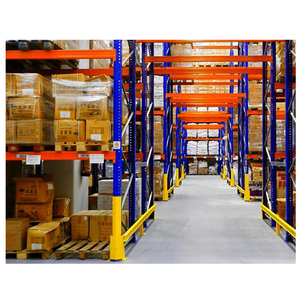
Heavy Duty Boltless Steel Pallet Rack System Industrial Warehouse Storage Shelves Metallic Heavy Duty Industrial Shelving
Interlocking tear-drop or diamond-slot upright systems permitting rapid field assembly without specialized fasteners.
Get CatalogWhy Top Global Brands Partner with China Rack Manufacturers
Chinese steel manufacturing leads the world in metallurgical scalability, automated roll-forming precision, and chemical surface coating technology. As a direct enterprise supplier, our manufacturing infrastructure leverages advanced structural analysis software, continuous cold-roll forming mills, and robotic laser-welding cells to ensure world-class performance.
Certified Metallurgy & Structural Steel Grade
We exclusively utilize prime structural steel feeds from top mills (BaoSteel, ShouGang) conforming to Q235B and high-yield Q355B standards. Every batch undergoes tensile testing, yield point analysis (up to 355 MPa), and impact resistance verification, surpassing standard international rack design requirements.
Seismic-Aware FEA Simulation
Each racking layout undergoes Non-Linear Finite Element Analysis (FEA) simulating real-world seismic ground accelerations (complying with NEC-SE-DS, ANSI MH16.1, and EN 16681). Upright profiles, baseplate anchoring, and beam-to-column connector teeth are optimized to resist dynamic sway and shear buckling.
Advanced Anti-Corrosion Coating
To resist harsh coastal air (e.g., Guayaquil, Manta ports) and sub-zero cold room condensation (-30°C), components pass a 16-stage chemical pre-treatment and continuous automatic electrostatic epoxy-polyester powder coating process, verified through 500-hour salt spray testing.
Full-Spectrum Material Handling & Storage Engineering
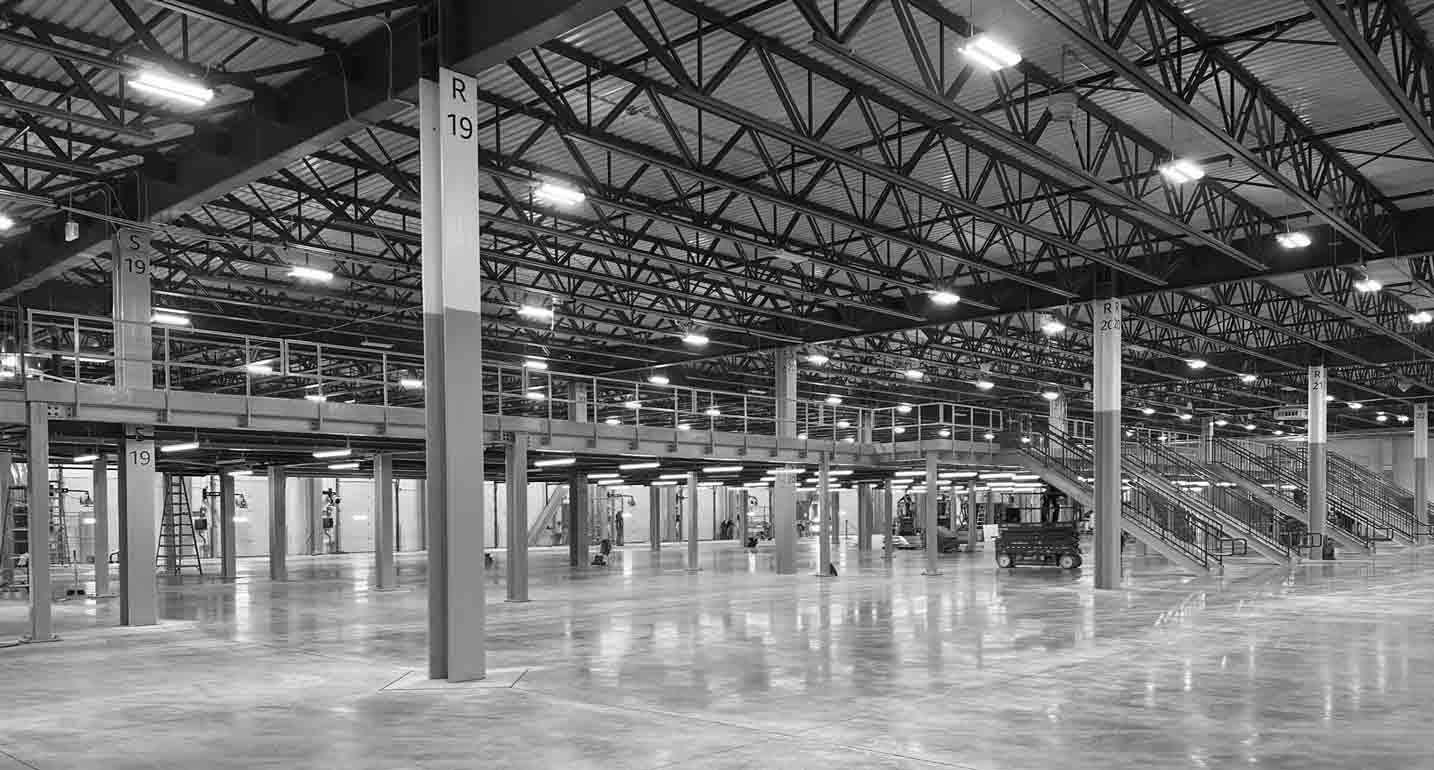
Modern distribution centers require more than just static pallet frames. They require seamless integration between structural racking, heavy-duty floor mezzanines, packaging machinery, and automated material handling equipment.
- Structural Mezzanines: Double or triple available floor footprint for assembly or order picking.
- AS/RS & Vertical Lifts: Direct interface with automated crane modules and shuttle carts.
- Dock & Packaging Protection: Impact post protectors, rack wire decking, and pallet wrapping lines.
Future Trends in Global Industrial Storage Procurement
Procurement directors sourcing industrial rack systems from China are moving beyond basic cost-per-pallet-position calculations. The global industrial storage landscape is undergoing radical technological shifts that buyers must incorporate into project specifications.
1. AGV & AMR Autonomous Integration
Standard forklift aisles (3.5m–4.2m) are rapidly giving way to autonomous guided vehicles (AGVs) and autonomous mobile robots (AMRs). Modern rack procurement demands tighter profile tolerances (±0.5mm), flush baseplate embedding, and floor guide rail integrations to enable robotic picking precision without physical human intervention.
2. Cold-Chain & High-Density Shuttle Automation
With global cold storage logistics expanding rapidly for seafood, fresh produce, and biopharmaceuticals, dense 4D radio-shuttle pallet racking is replacing traditional drive-in racking. Automated shuttle carts operate effortlessly down to -28°C inside specialized pre-galvanized rack lanes, maximizing warehouse cube utilization while reducing energy loss.
3. Stringent Seismic Mandates & Base-Isolation Tech
Global logistics hubs located along earthquake zones (such as South America's Pacific Ring of Fire or Asia-Pacific fault lines) now require dynamic seismic rack design. Procurement trends focus on heavy-gauge baseplates, high-ductility structural steel (Q355B), and anchored base-isolation dampeners that absorb lateral ground accelerations without rack collapse.
4. Modular & Boltless Fast-Deployment Architecture
E-commerce fulfillment operators require warehouse agility. Modern pallet rack design utilizes toolless, boltless drop-lock connector pins with safety locks. This allows facility operators to reconfigure beam elevations in 55mm or 75mm increments without structural downtime or specialized welding work.
Industrial Storage Rack Selection Guide
Comparing structural performance, picking speed, floor space utilization, and application suitability across major industrial racking configurations:
| Racking System Type | Floor Space Utilization | SKU Selectivity | Max Load / Level | Typical Industrial Application | Handling Equipment Required |
|---|---|---|---|---|---|
| Selective Pallet Rack | 40% - 50% | 100% (Direct Access) | Up to 4,500 kg | General Warehousing, FMCG, 3PL Distribution | Standard Counterbalance / Reach Truck |
| Drive-In / Drive-Through | 75% - 85% | 20% - 30% (LIFO/FIFO) | Up to 1,500 kg/pallet | Cold Storage, Frozen Seafood, Homogeneous Cargo | Deep-Reach Forklift Truck |
| Heavy Cantilever Rack | 60% - 70% | 100% (Unobstructed) | Up to 6,000 kg/arm | Steel Pipe, Lumber, Aluminum Profiles, Bar Stock | Side Loader / Specialized Forklift |
| High-Bay Mezzanine Platform | 150% - 300% (Multi-Tier) | 100% (Manual Pick) | 300 - 1,000 kg/m² | Auto Spare Parts, E-Commerce Picking, Garment Hubs | Conveyors, Freight Lifts, Hand Carts |
| Pallet Flow / Push-Back | 70% - 80% | 50% - 60% (LIFO/FIFO) | Up to 2,000 kg/lane | Food & Beverage, Expiry-Sensitive Goods | Standard Gravity-Flow / Reach Truck |
| Automated AS/RS Crane Rack | 85% - 95% | 100% Automated | Up to 3,000 kg/cell | High-Density High-Bay Automation (>25m Height) | Automated Stacker Cranes & Shuttles |
Engineering, Custom Fabrication & Field Installation
Our integrated engineering service spans initial site CAD layout design, structural calculation checks, OEM factory production, global ocean transport packing, and field installation supervision.
Custom Engineering & CAD Layouts
Comprehensive building survey analysis, clear-height evaluation, sprinkler clearance checks, and slab load distribution analysis performed prior to production.
High-Density Integrated Layouts
Combining heavy pallet storage with automated conveyor tracks, pick-to-light shelf modules, and safety wire mesh decking for maximum throughput.
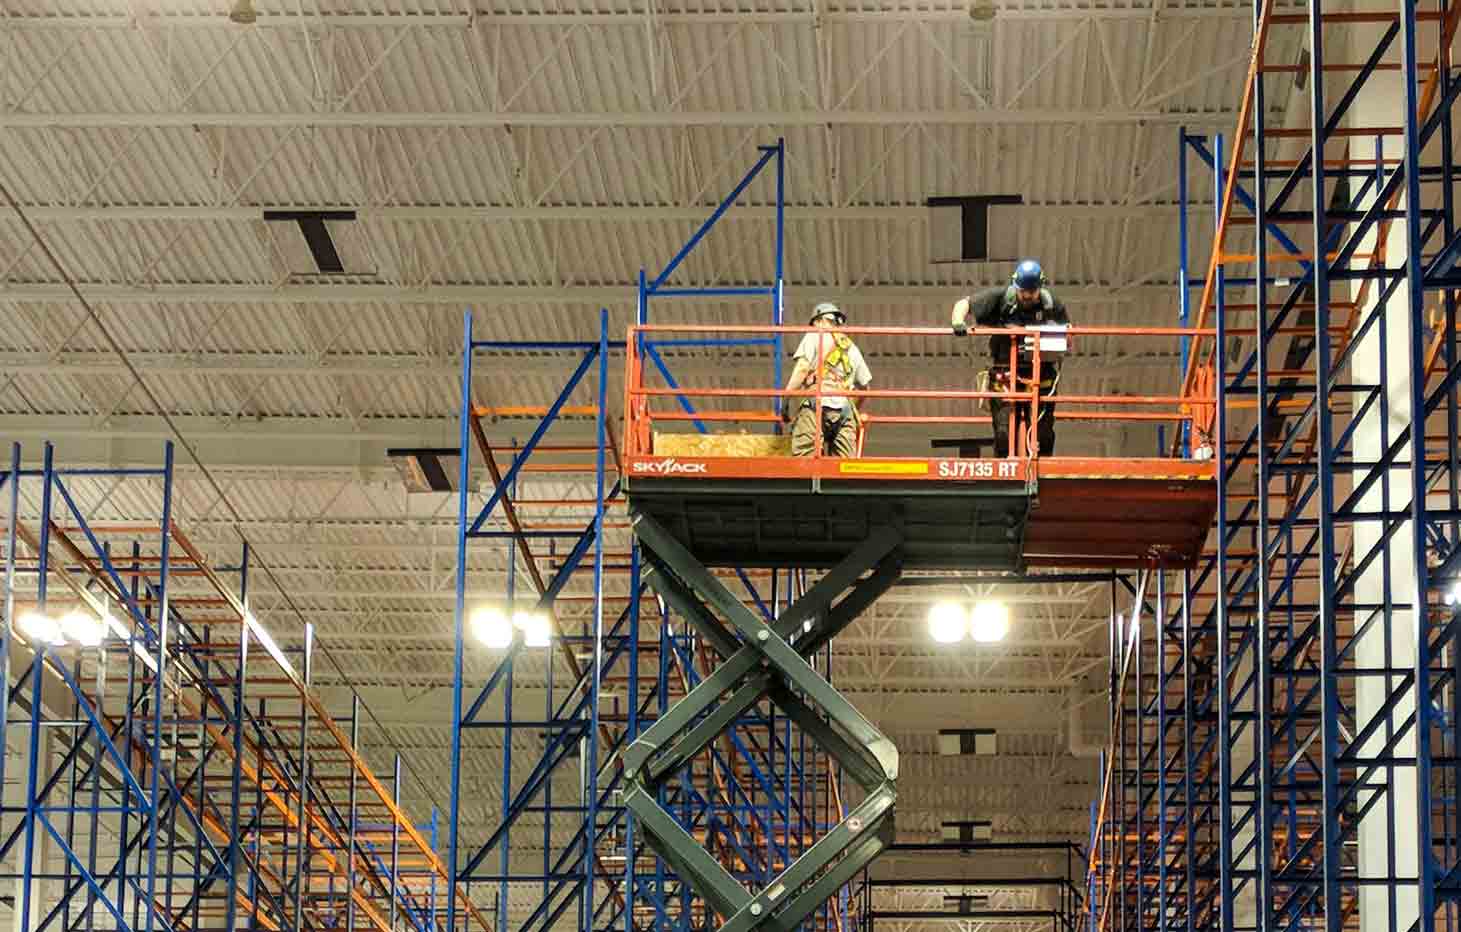
Global Field Installation Support
Certified field installation supervision, anchor expansion bolting, vertical plumb alignment, and safety signage compliance checks worldwide.
Frequently Asked Questions for Sourcing Industrial Racks from China
Clear technical answers to help procurement managers and warehouse engineers evaluate Chinese rack manufacturers with confidence.
Why source heavy-duty industrial storage racks directly from a Top China manufacturer?
How do China rack manufacturers ensure structural safety and seismic compliance?
What is the difference between Q235B and Q355B structural steel grades in pallet racking?
What protective surface finishes are recommended for coastal or cold-storage environments?
What information is required to receive a formal structural rack design and factory quote?
- Warehouse floor plan drawing showing clear height under sprinklers/trusses, column grids, and doors.
- Pallet load specification: Width × Depth × Height (including product) and maximum weight per pallet.
- Material handling equipment specs: Forklift model, maximum fork elevation height, and required operating aisle turning radius.
- Site geographic location for seismic zoning and slab concrete thickness assessment.
How are high-bay racks packaged and shipped to prevent damage during ocean container transit?
Our 6-Stage Engineering & Delivery Process
From initial architectural blueprint evaluation to final load certification, we maintain strict quality control at every phase:
Layout Consultation
We analyze your throughput requirements, SKU density, pallet load dynamics, and forklift aisle constraints to determine optimal racking geometry.
FEA Structural Calculation
Our structural engineers perform Finite Element Analysis checks verifying beam deflection limits, column buckling safety, and seismic ground shear compliance.
Precision Manufacturing
Automated cold-roll forming mills shape certified Q235B/Q355B steel profiles followed by robotic claw welding and 16-stage powder coating.
Quality Control Testing
Rigorous pre-shipment testing includes beam weld ultrasonic checks, coating thickness measurement, and destructive load-to-failure sampling.
Global Logistics & Freight
Container space optimization plans maximize tonnage capacity per 40HC container while preventing surface abrasion during sea transit.
Site Handover & Care
We supply detailed assembly blueprints, torque specs, load capacity plaques, and periodic inspection guides for facility safety officers.
Request Your Custom Warehouse Layout & Direct Factory Quote
Partner with a top China industrial rack storage manufacturer. Contact our structural engineering team today to receive CAD layouts, structural calculations, and a competitive factory-direct quote.